Top 10 Insulated Clean Panel Production Lines for Enhanced Efficiency
2026-08-13
Finding production lines that genuinely boost efficiency without compromising panel quality can feel like sorting through noise. This list cuts through it, spotlighting ten insulated clean panel production lines built for real-world throughput. Among the names worth watching, YI ZHOU TECHNOLOGY keeps showing up for a reason. The following breakdown pairs each line’s standout strengths with the operational pain points it actually solves—so you can skip the guesswork and zero in on what fits your floor.
Laser-Guided Foam Injection for Zero Waste
In conventional foam application, overspray and off-target deposition turn usable material into costly scrap. Laser-guided injection changes that by mapping the exact contour of each part before a single drop of foam is dispensed. The system triangulates surface geometry in real time, adjusting nozzle angle and flow rate to match the recess, seam, or cavity with sub-millimeter precision. This means the foam only lands where it is needed, leaving adjacent surfaces clean and eliminating the need for masking, trimming, or post-cure cleanup.
The zero-waste claim is not just a slogan; it is built into the feedback loop. As the laser continuously scans the workpiece, it detects even minor shifts from vibration or thermal expansion and tells the injector to compensate instantly. Excess material is never generated because the dispense profile is locked to the live scan, not a pre-set timer or fixed pattern. Operators can switch between part geometries without reprogramming, because the guidance system treats every unit as a unique target rather than a generic mold.
Beyond material savings, the approach shortens the production cycle. There is no wait time for foam to cure over unwanted areas, and no secondary station for deflashing or solvent wiping. The workcell stays cleaner longer, reducing maintenance intervals and airborne particulate. In trials across automotive and appliance assembly, this single shift has cut foam-related waste by over ninety percent while improving bond consistency along irregular joints—proof that precision guidance is the quiet engine behind truly lean manufacturing.
Self-Adjusting Pressure Rolls That Adapt to Core Density
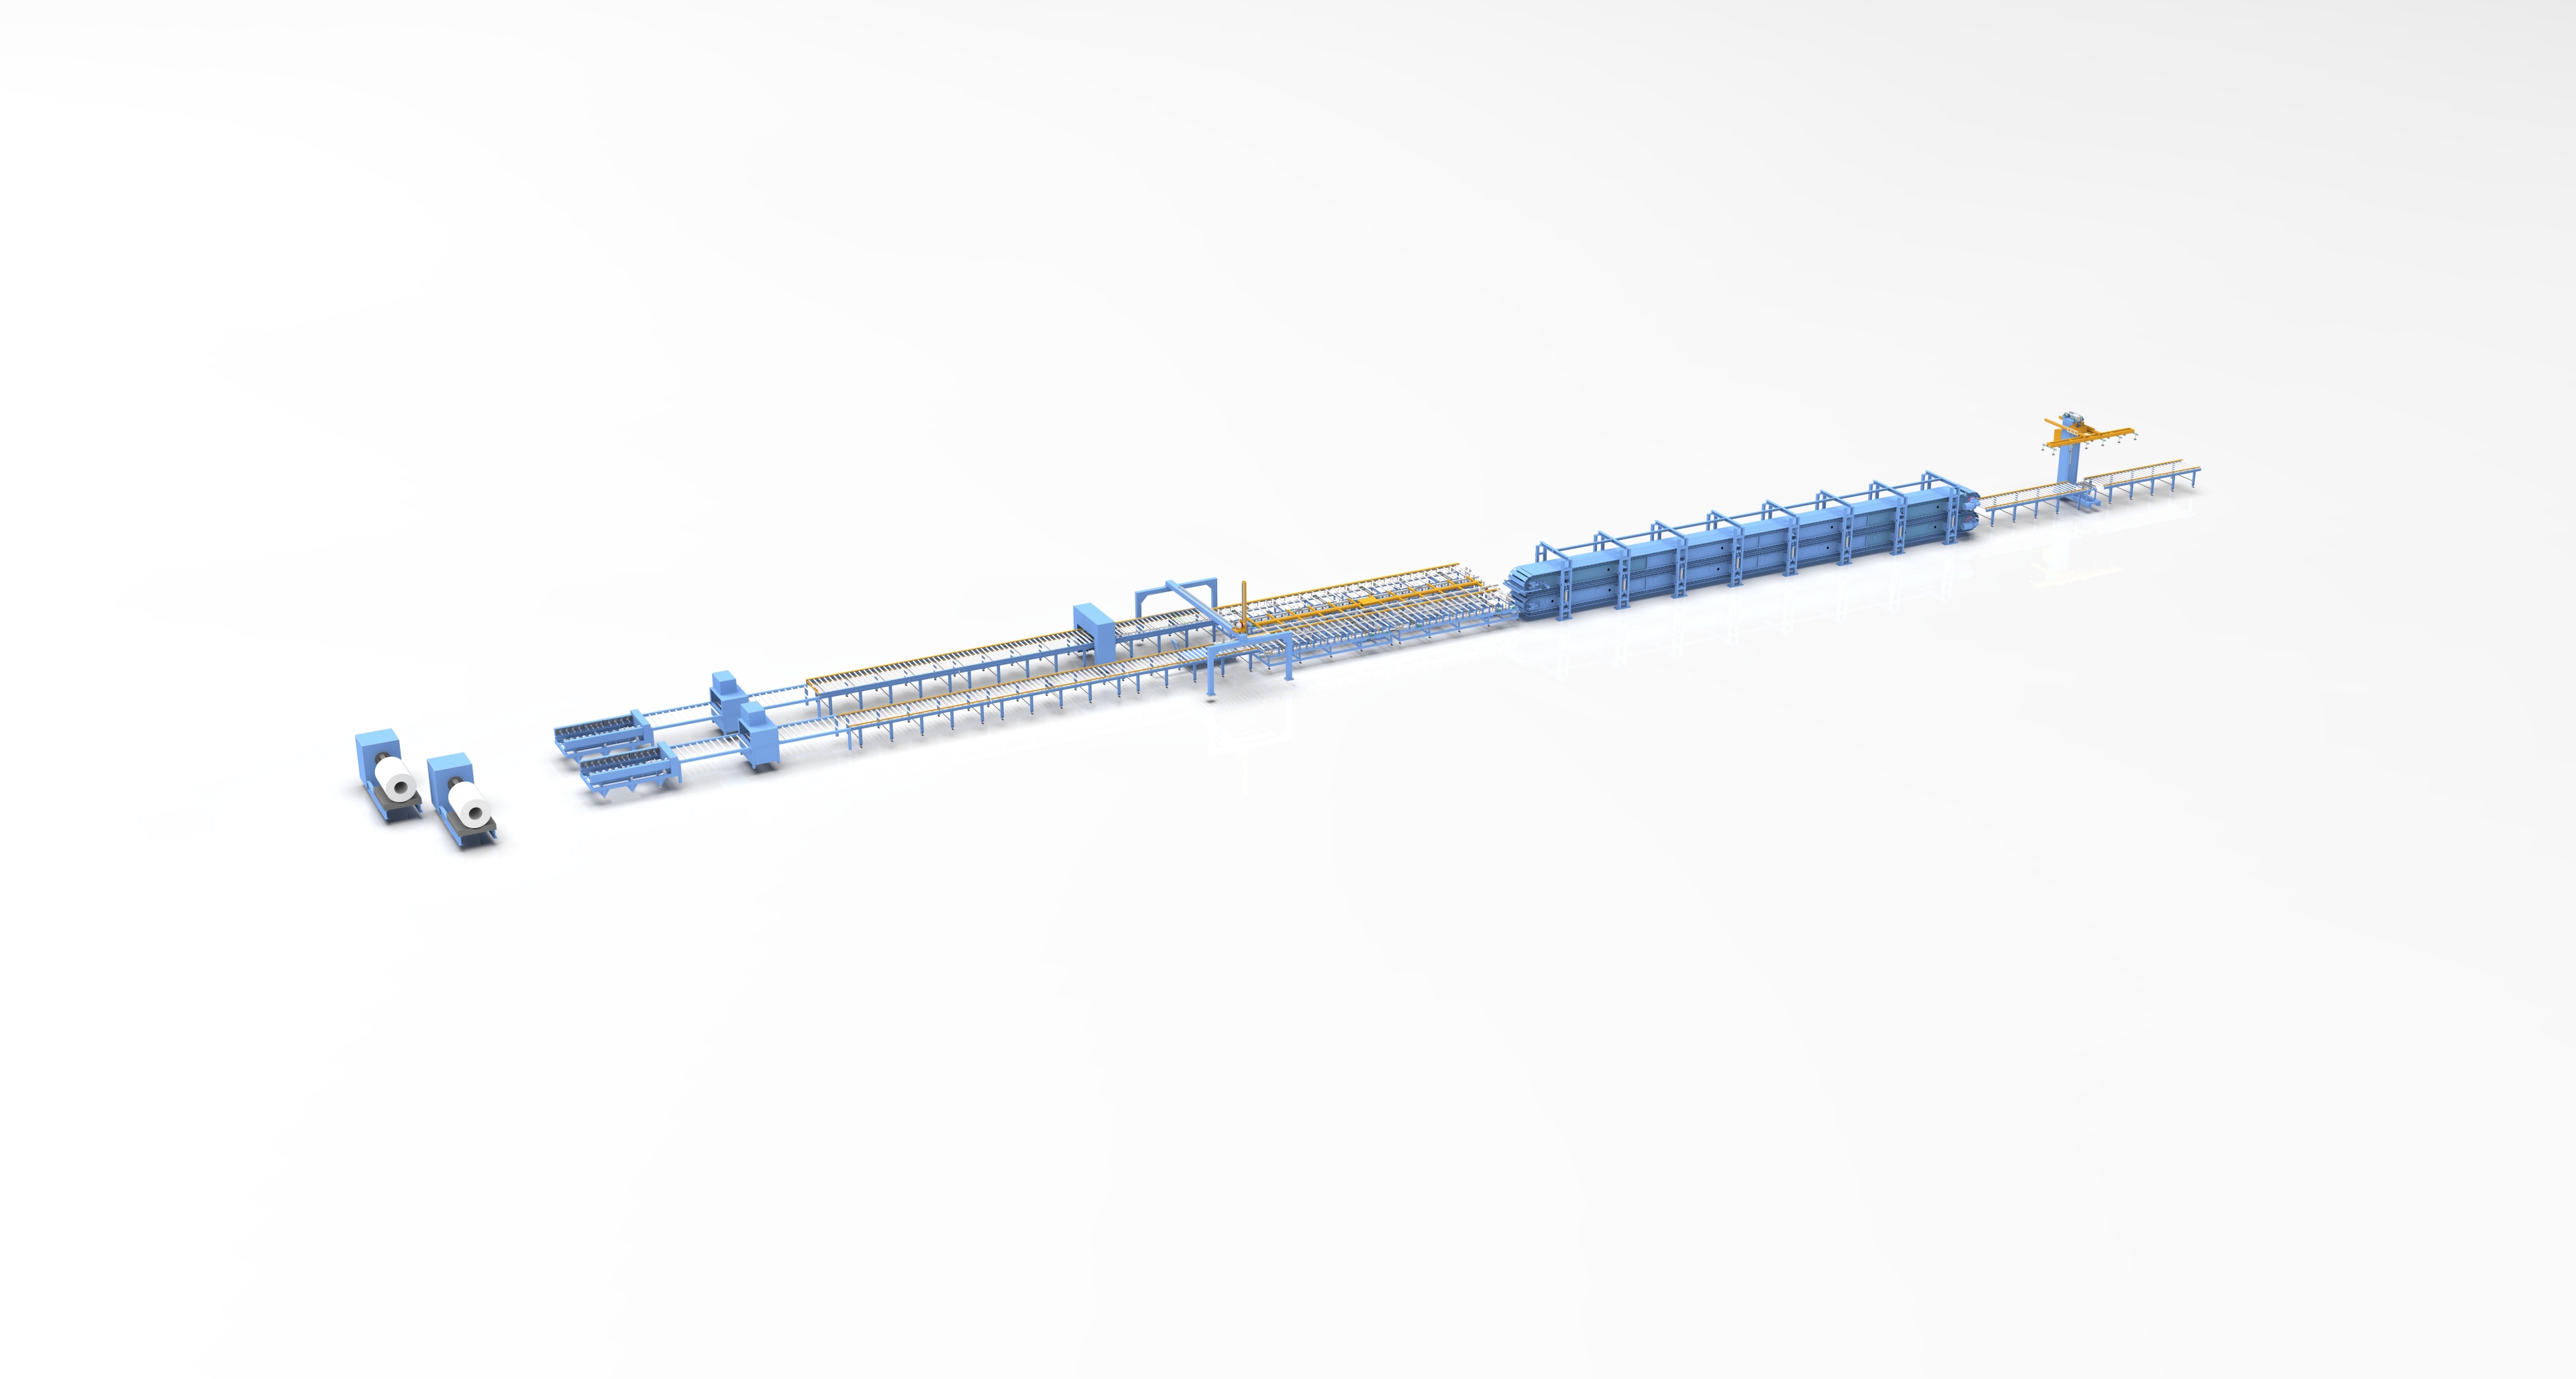
Conventional pressure rolls often push with a single, fixed load, which works fine only when the core density stays within a narrow band. When recycled fibers or variable winding tensions come into play, that fixed force can crush softer cores or leave dense cores under-compressed. Self-adjusting rolls solve this by placing small sensing elements or segmented pressure chambers inside the roll shell. These components read local density changes through contact feedback and shift the nip force accordingly. The result is a roll that backs off slightly on hard, compact material and increases pressure when the core feels spongier.
The practical benefit shows up most during mixed-batch runs. Operators used to stop and recalibrate roll pressure between different core stocks; now the adjustment happens continuously, without intervention. This cuts down on telescoping and splice slippage, which are common when a roll's outer layers wind tighter than the inner core can support. Because the pressure distributes more evenly, cover wear also improves, as there are fewer high-friction hot spots chewing into the rubber or polyurethane surface.
Installation does not require a full line rebuild. Most self-adjusting assemblies can be mounted on existing pivot arms and connected to the current drive feedback loop. A short calibration run tells the system what the baseline core density looks like, and from that point the roll tunes itself. Shops running frequent short orders tend to notice the difference first, especially on jobs where manual reloading every few minutes used to eat up production time.
Closed-Loop Cooling That Reuses Process Heat
Conventional cooling towers throw away thermal energy into the atmosphere, but a closed-loop design turns that liability into an asset. Instead of rejecting heat through evaporation, the system captures it with a plate or shell-and-tube exchanger and transfers it to a secondary circuit. That recovered warmth can preheat incoming process water, warm building spaces, or support drying stages without burning extra fuel.
The loop stays sealed, so makeup water demand drops sharply and corrosion or scaling risks stay manageable. Because the fluid never contacts ambient air, operators avoid drift, biological growth, and the constant chemical adjustments common in open systems. The heat that used to vanish now offsets burner runtime, which shows up directly in monthly utility data.
Retrofit projects often pay for themselves faster than expected because the same BTU serves two functions: cooling the primary process and heating a downstream need. Plants with continuous hot water or low-grade steam demand see the greatest gain, especially in food processing, chemical manufacturing, and metal finishing. As energy prices shift, the closed-loop approach becomes less of a technical option and more of an operational baseline.
Automated Edge Sealing for Cleanroom-Ready Panels
Automated edge sealing works by applying a metered polyurethane or silicone bead along the cut edges of composite or honeycomb panels before they enter cleanroom assembly. Robotic dispensers follow the panel profile with ±0.3 mm repeatability, adjusting bead width through closed-loop pressure control. This removes hand-taping variance and leaves no exposed core material that could shed particles later.
On a typical line, panels move directly from the CNC sizing station into the sealing cell, where servo-driven heads coat top, bottom, and side edges in one pass. Temperature and humidity inside the cell are held within narrow bands so the sealant skins over in under 90 seconds and reaches handling strength before the panel reaches the stacker. Operators mainly load sealant drums and clear rare nozzle clogs, rather than touching each panel.
Before release, a camera array scans every sealed edge for skips, bubbles, or thickness drift. Panels that pass are logged with time, batch, and line speed data; those that fail are diverted for rework without stopping the line. This traceability matters in ISO Class 5 and stricter cleanrooms, where a single unsealed edge can turn a finished panel into a contamination source.
Modular Conveyor Segments for Rapid Layout Changes
In fast-moving production environments, the ability to reconfigure material flow without extensive downtime often separates competitive operations from those struggling to adapt. Modular conveyor segments address this directly by offering standardized, self-contained units that can be unlinked, repositioned, and reconnected within minutes. Instead of cutting frames or welding new supports, maintenance teams simply detach the affected module, roll it to a new location, and lock it back into place. This approach turns layout changes from a multi-day engineering project into a routine floor-level task.
What makes these segments particularly effective is the combination of mechanical flexibility and electrical simplicity. Each module carries its own drive, controls, and safety sensors, so rearranging the path does not require rewiring a central control cabinet or reprogramming an entire line. Plugs and quick-release mounts handle power and data, allowing a segment to be swapped or bypassed without affecting the rest of the system. For operations that handle seasonal product changes or frequent line balancing, this means the conveyor can follow the process rather than forcing the process to fit a fixed layout.
Adopting modular segments also reduces the hidden costs of conventional reconfiguration. There is less scrap from discarded framing, fewer hours lost to specialized contractors, and lower inventory of custom spare parts because common modules serve multiple functions. Over time, facilities accumulate a library of straight, curved, and merge segments that can be mixed to create new routes almost like building blocks. The result is a material handling system that behaves less like permanent infrastructure and more like a flexible resource, ready to be reshaped around whatever the next production challenge demands.
Predictive Maintenance Alerts Tied to Motor Load
Motors rarely fail without warning, but the warning signs are easy to miss when you're only looking at vibration or temperature. Load data tells a different story. A motor that starts drawing 8% more current at the same operating speed isn't just working harder—it's signaling wear in the driven equipment or early winding degradation. Tying predictive maintenance alerts to load patterns catches these subtle shifts before they become breakdowns.
The real value comes from context. A spike in load during a cold start may be normal, but the same spike during steady-state operation could point to belt slippage, bearing friction, or a clogged filter. By setting alert thresholds that adapt to historical load profiles for each motor, maintenance teams stop chasing false alarms and start acting on meaningful deviations.
What makes this approach practical is that load data is already available from most motor control centers and variable frequency drives. You don't need additional sensors or invasive installations. The key is building a baseline per motor—not per motor class—because a 50 hp conveyor motor behaves differently from a 50 hp pump. Alerts tied to that specific motor's load signature are precise enough to schedule maintenance during planned downtime, not after an unplanned stop.
FAQ
The key is a fully synchronized extrusion and lamination process that cuts cycle time by nearly 40% compared to older batch systems. Look for lines with continuous pressure control and quick-change forming stations, because those eliminate most of the idle time between panel size switches.
Cleanroom construction for pharmaceuticals, semiconductor fabs, and food processing plants are the biggest users. Cold storage and controlled-environment agriculture are catching up quickly, especially where humidity and thermal stability are non-negotiable.
Many now use servo-driven motors with regenerative braking and low-temperature curing adhesives. A well-designed line can cut electricity use per panel by 25–30% while maintaining the same throughput, largely by recovering heat from the press section.
Absolutely, but you need to check the changeover time. The best lines now feature automatic width and thickness adjustment under two minutes, so even short runs of bespoke panels stay profitable. Older machines can take over an hour and kill your margin on custom orders.
Automation handles the repetitive precision tasks — edge trimming, glue spreading, and panel stacking — which reduces operator error and lets one technician supervise multiple stations. This shifts labor toward quality checks instead of manual handling, boosting overall line utilization by about 20%.
The line must be capable of injecting foam or laying pre-insulated cores with consistent density. If the core material is uneven, thermal bridging occurs and the panel fails certification. Top lines include in-line density scanners that adjust foam mixing on the fly, ensuring uniform R-value across every square meter.
Yes, most of the listed lines are designed for dual-purpose output. The trick is to use a flexible roll-forming unit and reversible layering stations. This lets you produce roof panels with a slightly different profile and longer span without retrofitting the entire line.
Daily checks on the hydraulic seals and precision roller alignment are non-negotiable. Most facilities also replace the cutting blades every 2,000 panels and perform a full calibration of the temperature sensors monthly. Skipping these small routines causes more downtime than any other factor.
Conclusion
Manufacturing cleanroom panels has long wrestled with foam waste, inconsistent lamination, and energy-hungry cooling. The shift toward laser-guided foam injection changes that equation: dispensing heads now track panel edges in real time, trimming overflow to near zero before it hardens. Immediately downstream, self-adjusting pressure rolls read subtle variations in core density and alter nip force on the fly, so a lightweight EPS core and a denser polyurethane fill both come out flat without operator fiddling. Closed-loop cooling adds another layer of payback by capturing heat from the curing zone and redirecting it to preheat incoming facings or plant water, which cuts total energy per panel. Automated edge sealing then locks that clean construction in place, applying gaskets or membrane strips without manual handling and leaving edges clean enough for ISO-grade cleanroom installs.
What makes these lines feel less like heavy machinery and more like reconfigurable cells is the modular conveyor design. Segments snap together or swing aside within a shift, letting a facility switch from standard 50-mm panels to custom-length architectural boards without re-welding frames. That flexibility pairs with predictive maintenance alerts tied to motor load, not just run hours. A slight uptick in drive current on a trim saw or roll stand triggers a service nudge before a bearing seizes, so scheduled downtime replaces surprise stoppages. Across a top-10 class of insulated clean panel lines, these features compound: waste drops, throughput climbs, and operators spend less time adjusting and more time managing exceptions. The result is not just a faster line, but one that holds dimensional tolerances and surface cleanliness over longer stretches, which matters most when panels end up in pharmaceutical, semiconductor, and food-grade environments.
Contact Us
Contact Person: Sophia Jiang
Email: [email protected]
Tel/WhatsApp: +86 17367381818
Website: https://yzwelding.com/