Film Sandpaper Company Unlocks Next-Level Abrasive Film Performance
2026-10-03
What if the abrasive film you reach for could suddenly cut cleaner, resist loading longer, and hold its edge through the toughest finishes? That question is moving from hypothetical to reality as one film sandpaper specialist breaks through familiar performance ceilings. In this post, we’re looking at how SHENZHEN SUN ABRASIVES is unlocking next-level abrasive film performance—and why that shift matters for anyone chasing faster, more consistent surface results.
What Actually Changes When the Film Gets Thinner
As the film thins past a few hundred nanometers, its optical behavior stops following bulk rules. Interference between reflections from the top and bottom surfaces becomes significant, producing color shifts that depend on thickness. Once the film drops below about a quarter of the wavelength of visible light, those colors largely disappear and the layer looks essentially transparent, because the path difference is too small to create strong constructive or destructive interference.
Mechanical integrity changes too. A thinner film has a higher surface-to-volume ratio, so surface forces and adhesion begin to outweigh internal stiffness. Films that hold their shape at fifty microns often become delicate, curling or crinkling at five microns unless supported. Permeability also tends to rise, since small defects and pinholes are more likely to span the full thickness, allowing gases and moisture to pass through more easily.
There is also a shift in how the film handles heat and electricity. Ultra-thin layers can scatter electrons and phonons more frequently at interfaces, lowering effective conductivity in some directions. Yet this same confinement can create new behaviors, such as quantum well effects in semiconductors or enhanced gas sensitivity in metal oxide films, making the loss of thickness not just a trade-off but a functional change.
Grain Bonding That Outlasts Standard Backings
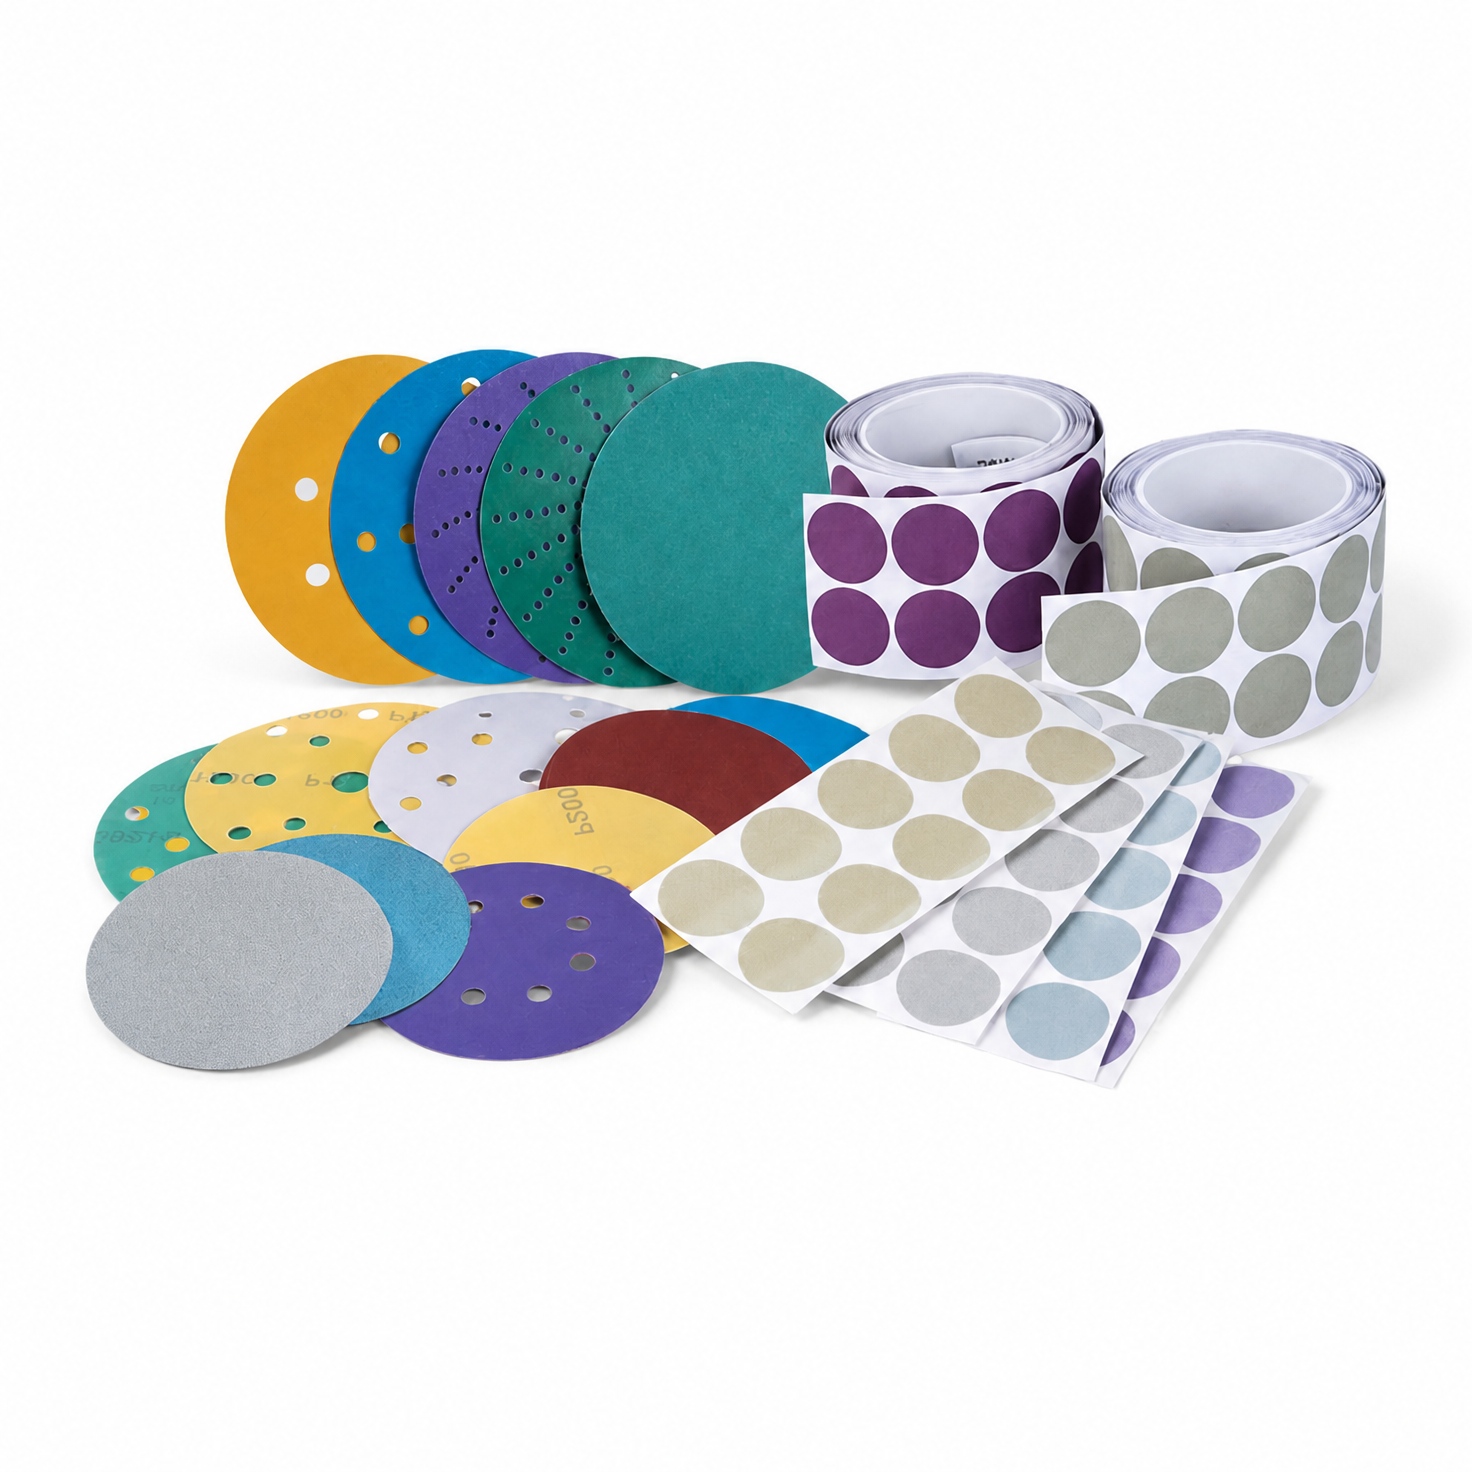
Most abrasives fail long before the grit wears smooth—the bond lets go. On standard backings, heat and flex work the grains loose after a short stretch, leaving shiny patches that slide instead of cut. This grain bonding is different: the abrasive is locked into a resin matrix that cures slowly, so each particle sits deeper in the backing rather than just coating the surface.
The practical difference shows up on curved edges and tight corners, where a stiffer backing would crack and a weaker bond would shed. Here, the grain remains anchored as the backing flexes, which means you spend less time swapping sheets and more time getting an even scratch pattern. It also holds together when the material builds up heat—something that quickly kills standard resin bonds.
Over the life of a sheet, that adds up. You get to use more of the abrasive you paid for, and the backing doesn't fray into the work. For anyone who has watched a fresh disc turn smooth in minutes, this kind of bond is the fix that isn't immediately visible but is easy to feel.
Why Operators Report Fewer Passes on Hard Metals
On softer alloys, abrasive grains tend to plow into the surface and get loaded with smeared metal almost immediately. That buildup hides the cutting edges and forces the operator to make extra passes just to get back to clean material. Hard metals behave differently: instead of smearing, they fracture into small, brittle chips that clear out of the contact zone. The abrasive stays sharp and exposed, so each pass removes actual stock rather than just rubbing over a clogged surface.
The heat story also changes when the workpiece is hard. Softer metals generate a lot of friction and can glaze the abrasive, especially under moderate pressure. Hardened steels and carbides shed heat more quickly into the chip rather than into the tool or the part. That keeps temperatures lower at the cutting points and reduces the chance of a melted or deformed smear layer. With less glazing, operators find they can push a little harder per pass and still get a consistent finish, which naturally cuts down the total number of passes.
There is also a practical side to it. Hard metals rarely require the light, repetitive skimming that soft, gummy materials demand. Once the right abrasive and feed rate are dialed in, the material removal rate stays steady until the job is done. Fewer passes not only shorten cycle time, but also reduce wear on fixtures and machine slides because there is less back-and-forth movement under load. That is why experienced operators often look forward to hard metal jobs, even if the material itself is tougher to grind.
The Role of Film Flexibility in Complex Contours
On deeply sculpted panels, film flexibility determines whether the material can reach into sharp recesses and wrap around tight radii without pulling away from the surface. A film that resists stretching will bridge across concave channels, leaving air pockets and exposed edges that become failure points. More pliable films, by contrast, yield under tension and settle into the contour rather than fighting it.
This matters most during the initial stretching phase, where uneven force is applied across compound curves. A flexible film redistributes that stress instead of concentrating it along a single ridge or valley. The result is fewer wrinkles, less need for relief cuts, and a cleaner transition from flat sections into curved details.
Over time, that same flexibility continues to pay off. Body panels flex with temperature changes and road vibration, and a rigid film may crack or lift at the edges of a recess. Pliable films absorb those small movements, keeping adhesion intact even on surfaces that bend in more than one direction.
Cutting Heat, Not Corners, in High-Pressure Sanding
High-pressure sanding generates friction that can push surface temperatures past 400°F on steel, but the real damage isn't the heat itself—it's what the heat does to the abrasive and the workpiece. Resin bonds start to soften, grit dulls prematurely, and thin-gauge metals warp or discolor. The temptation is to back off the pressure or switch to a finer grit to keep things cool, but that's exactly the corner-cutting that shows up later as uneven stock removal or a finish that needs rework. The goal is to cut the heat, not the productivity.
A more direct route is to rethink the abrasive contact zone. Using a structured abrasive with precisely spaced pyramidal grains reduces friction by allowing swarf to escape instead of being trapped between the grit and the surface—trapped swarf is a major hidden heat source. Pair that with a stearated coated abrasive or a ceramic grain that fractures at lower pressure, and you get a cooler cut without backing off the force. On wide-belt machines, adding a graphite-coated platen or a compressed-air knife just after the contact roller pulls heat away before it soaks into the workpiece.
The payoff shows up in edge sharpness and belt life. One shop grinding 304 stainless switched from a standard alumina belt to a ceramic structured belt and saw surface temperature drop by roughly 60°F while removing the same stock per pass. The belts lasted three times longer because the resin bond never reached its softening point. That's the difference between sanding hot and sanding smart—less heat, same cut, no corners left behind.
A Closer Look at the Company's Proprietary Resin System
Most resin systems on the market lean heavily on standard epoxy or polyester chemistry, which means they inherit the same trade-offs: brittleness under impact, sensitivity to moisture, or a narrow curing window. This company's proprietary resin is built from a modified polymer backbone that deliberately breaks that mold. Rather than chasing a single headline property, the formulation balances flexural strength, chemical resistance, and thermal stability in a way that feels almost self-correcting during real-world use—edges stay sharp, bonds don't creep, and surfaces shrug off solvents that would haze a conventional finish.
What stands out in day-to-day handling is how forgiving the system is before cure. The viscosity stays low enough to wet out dense fiber packs without vacuum assistance, yet it doesn't puddle or drain unpredictably on vertical sections. Pot life runs longer than typical fast-set resins, but the transition from tack-free to full hardness happens quickly once the exotherm peaks—so technicians aren't stuck waiting half a shift between layup and demolding. There's also a noticeable absence of that sharp, nose-stinging amine odor common to many industrial resins, which matters more than spec sheets usually admit.
Long-term, the resin's crosslink density is tuned to avoid the micro-cracking that often appears after repeated thermal cycling. Samples pulled from field trials show no measurable loss in interlaminar shear strength after hundreds of freeze-thaw swings, and the surface retains its gloss without waxing or post-curing. For anyone who has watched a cheaper system turn chalky or delaminate at the edges, this is the difference between a material that simply meets a datasheet and one that holds its character when the job gets rough.
FAQ
The team moved to a dual-layer resin system that cures at a lower temperature, letting the abrasive grains sit taller and cut cooler. That change alone reduced heat buildup by about a third during long sanding runs.
Fine finishing on automotive clear coats and composite aerospace panels are the obvious winners. We also see strong demand in solid surface fabrication, where scratch depth and swirl marks have been persistent pain points.
We added a zinc stearate dry lubricant into the top coat and spaced the grain clusters more aggressively. The result is that aluminum and softwood dust clears out before it can load the surface, which keeps the cut rate steady far longer.
In our controlled panel sanding tests, the new film lasted between 2.5 and 3 times longer than a conventional aluminum oxide film of the same grit. The edge retention is especially noticeable on hard maple and high-solids primer.
It is built on a thin polyester backing with a controlled stretch factor, so it wraps curves without cracking. We have customers using it both on orbital sanders and with soft interface pads for concave moldings.
The launch covers P80 through P2000 in rolls, discs, and sheets. A wider jumbo roll format is coming later this quarter for automated sanding lines that need fewer changeovers.
We ran third-party abrasion tests per ISO 21948 and also did side-by-side field trials with two custom cabinet shops. The lab data showed lower surface roughness after the same number of strokes, and the field crews reported less hand fatigue from reduced pressure needed.
Conclusion
Film Sandpaper Company has reworked its abrasive film lineup around a thinner, more uniform backing that changes how force reaches the cutting edge. Instead of losing energy to a thick, spongy carrier, the slimmer film transfers pressure almost directly into the grain, which means operators spend less time working hardened steels and other tough alloys. The practical result is fewer passes to knock down a weld or blend a scratch, even on metals that usually punish standard abrasives. This isn't just a tweak to thickness; the film's flex makes it wrap around complex contours without creasing or skipping, so detail work on curved or recessed surfaces feels less like a fight.
The bigger shift comes from the bonding and resin system. The company's proprietary formulation locks each grain in place longer than typical backings, resisting the heat buildup that normally softens adhesives and sheds abrasive particles. Under high-pressure sanding, the film holds its edge and cuts cooler, which reduces loading and keeps the surface finish consistent from the first stroke to the last. By pairing that resin with a backing that flexes instead of fracturing, Film Sandpaper Company has created a film that behaves more like a sharp hand tool than a consumable, letting shops push harder without burning through discs or shortening the abrasive's usable life.
Contact Us
Contact Person: Amanda Wang
Email: [email protected]
Tel/WhatsApp: +86-13602569854
Website: https://www.sunabrasives.com.cn