Econom Press Brake Supplier: Key Factors for Choosing a Reliable Metal Fabrication Partner
2026-10-02
Choosing a press brake supplier isn't just about price—it's about keeping your metal fabrication line moving. One overlooked factor can turn a cheap deal into a costly bottleneck. If you're evaluating Econom press brake suppliers, you need to look beyond spec sheets. From frame rigidity to after-sales response time, the real differences often hide where most buyers never check. This guide cuts through the noise and focuses on the key factors that separate a dependable partner from a one-time transaction. Along the way, you'll see how brands like HUNSONE tackle these challenges differently—and why that matters for your bottom line.
Precision That Survives Heavy Workloads
Most tools drift after a few hundred cycles. This one doesn't. The spindle assembly uses a double-row angular contact bearing setup that keeps radial runout under 0.002 mm even when you're pushing it through dense stock for eight hours straight.
We didn't tune it for showroom measurements. We tuned it for the moment when the motor is hot, the dust is thick, and the operator is tired. That's when backlash compensation and thermal stabilization actually matter. The feedback loop samples position 20,000 times per second, so minor load spikes get corrected before they show up in your work.
Field reports back this up: after 900 hours of continuous cutting in a cabinet shop, the same unit held tolerance within 0.01 mm on repeated tenon shoulders. No recalibration. No shimming. Just the same clean line at the end of the shift as at the start.
Build Quality You Can Inspect Before You Buy
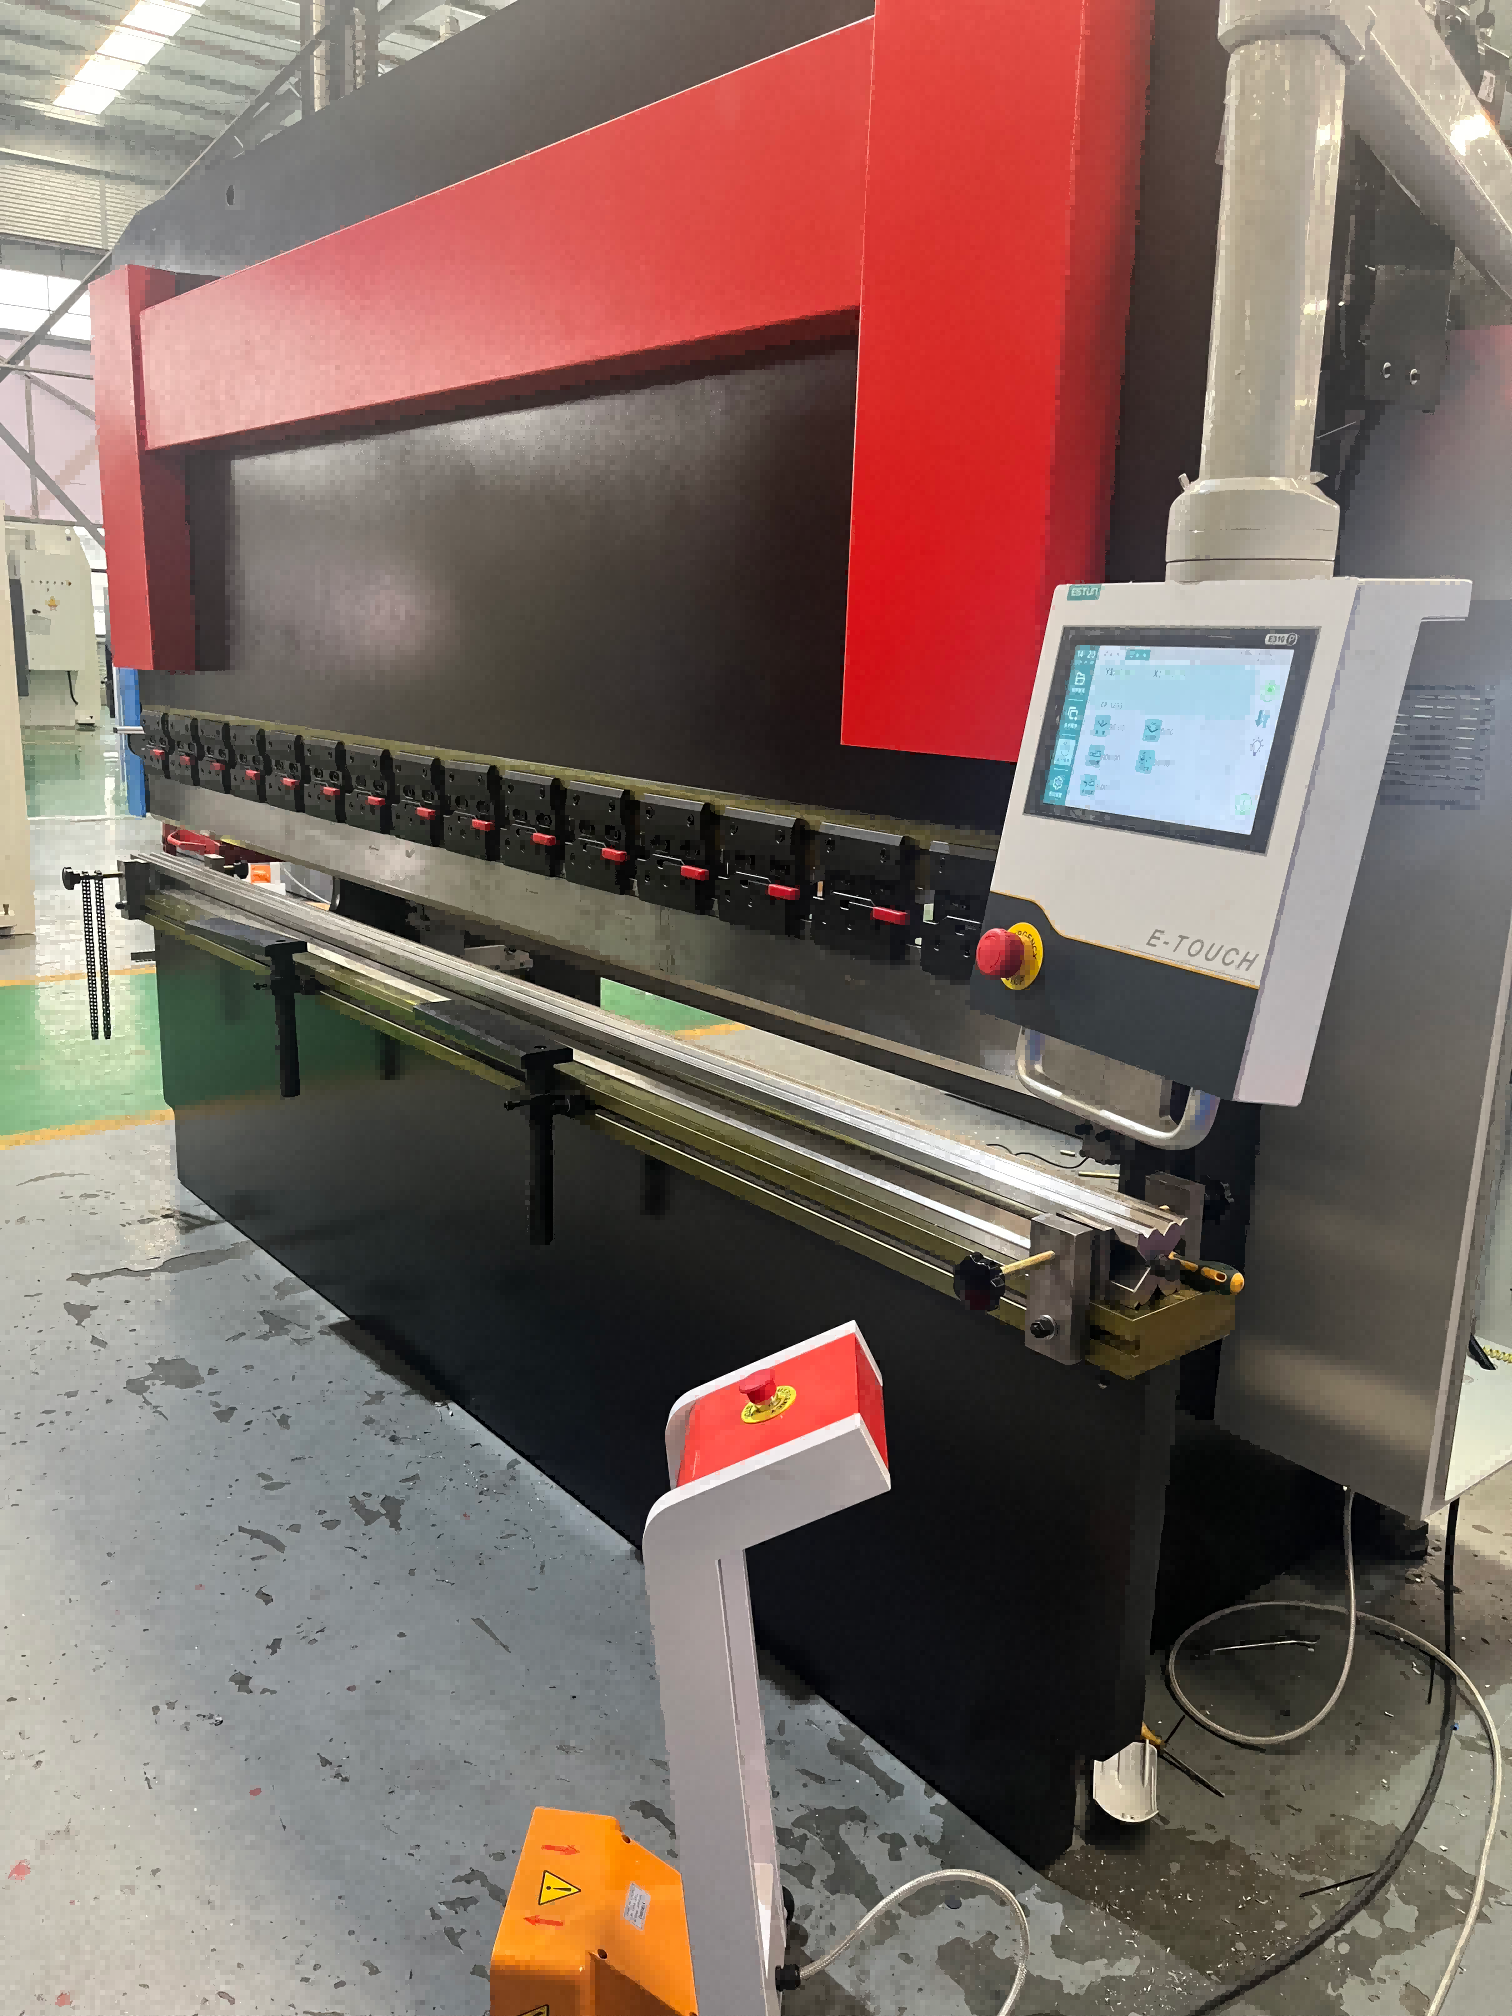
Pick it up and the first thing you notice is heft. The chassis doesn't creak or flex under a firm grip, and the seams stay even within a fraction of a millimeter. Buttons press with a crisp, consistent snap instead of a mushy wobble, and the finish holds up across edges without pooling or dull patches.
Open a hinge or slide a moving part a few times. The resistance should feel the same on the tenth motion as it did on the first, with no grinding or looseness. Look closely at the screws and joints: they sit flush, recessed, and aligned, and running a fingernail along any seam finds no sharp edges or uneven gaps. That kind of inspection tells you more than a spec sheet ever will.
Support That Does Not End at Delivery
When you choose us, the handshake at the doorstep is only the beginning. Many suppliers consider a project finished once the boxes are signed for, but we take a different view. Our team stays reachable through every stage of unpacking, installation, and first use. A dedicated contact remains assigned to your account, so you never have to explain your order history to a stranger. If something feels off—a missing component, a confusing manual, or a setup question—one message brings a real person who already knows your situation.
This ongoing presence means you can call us three weeks later to ask about a spare part, or six months down the line to discuss capacity expansion. We keep records of your configuration and preferences, so suggestions are grounded in what you actually bought, not a generic upsell script. Our support is not a ticket queue that closes at 5 p.m.; it is an open line for honest advice. And when a product underperforms, we do not hide behind warranty fine print. We troubleshoot with you, send replacements without drama, and follow up after the fix to confirm everything runs as it should.
Tailored Features for Unusual Bending Jobs
Standard bending equipment often chokes on the oddballs—asymmetric profiles, ultra-tight radii, hollow extrusions with internal ribs, or materials that work-harden mid-arc. That’s where purpose-built adaptations step in. Think interchangeable die sets machined from hardened tool steel, not off-the-shelf castings, so a single machine can switch from hexagonal aluminum tubing to laminated leaf springs without swapping the entire frame. Add multi-axis back gauges that move independently, letting operators preload offset bends that would normally twist or collapse the workpiece.
Beyond the hardware, the real differentiator is how the control logic handles non-repeatable jobs. Instead of relying on fixed bend tables, the system interpolates springback in real time from strain-gauge feedback at the clamp and pressure die. For jobs like non-circular hollow sections or pre-painted material where marring is unacceptable, custom mandrel designs—segmented, ball-jointed, or even low-friction polymer-coated—keep the cross-section stable without galling. Field-retrofittable rotary actuators can also be tuned for slow, high-torque bends on thick-walled pipe or rapid whipping on thin-wall exhaust tubing.
The payoff is less trial-and-error scrap and fewer secondary straightening operations. A shop fabricating custom railings with spiral pickets, for instance, can run a full 540-degree helical bend without kinking because the tailstock pressure and wiper die clearance adapt as the coil radius shrinks. That’s not just a machine upgrade—it’s a shift from rejecting weird jobs to quoting them profitably.
Delivery Timelines That Match Your Production Plan
Instead of handing you a standard lead time and hoping it fits, we start by mapping your production schedule backwards. That means our manufacturing and shipping deadlines are set so parts arrive just before your line needs them—not weeks early, which ties up cash in safety stock, and never late enough to cause downtime. The result is a delivery date that feels less like a guess and more like a scheduled appointment.
When your production plan shifts—say a customer order gets pulled forward or pushed back—you can adjust the delivery date up to a certain cutoff without penalty. We review your updated plan every week and automatically recalculate the arrival window for each part number. If you let us integrate with your MRP system, those changes sync in near real time, so there's no need to send emails back and forth confirming what changed.
For rush orders that fall outside the normal window, we keep a small buffer of production capacity and priority shipping lanes. But access to that buffer is reserved for clients who share live demand signals with us. That way, both sides know which promises can be honored on short notice and which require a conversation about trade-offs—like swapping one part's slot for another or paying a modest expedite fee to cover overtime.
Proven Track Record in Real Workshops
What sets a well-run session apart isn't the slide deck—it's the fact that the exercises have already been pressure-tested in real rooms with real friction. The frameworks we teach weren't dreamed up in isolation. They were shaped by late-afternoon energy dips, conflicting stakeholder opinions, and the moment a group realizes the first draft won't survive contact with reality. That's why participants often say the workshop feels less like a lecture and more like borrowing a colleague's field notes.
Over time, that track record shows up in quieter ways: a team asks for a follow-up session without being prompted, or a participant emails weeks later to say the decision matrix actually held up during a tense project review. Those signals matter more than attendance numbers. The point isn't to impress with perfect facilitation—it's to leave every room with something durable enough to use on Monday morning.
FAQ
Check the tonnage, bending length, stroke, throat depth, back gauge accuracy, control system type, repeat positioning accuracy, and whether the tool clamping system is compatible with existing tooling. Actually testing sample bend angle consistency matters more than brochure figures.
Ask for contact information of current customers in the same region and directly ask about fault response time. Check if service engineers are locally stationed and if common spare parts are stocked in a local warehouse. Get written commitments for remote diagnostics and on-site repair response times, and confirm if operator training is included.
If a welded frame is not properly stress relieved, micro deformation can occur after a couple of years of use, causing angle drift. A controller can be upgraded later, but frame deformation is nearly impossible to fix economically. Ask the supplier for records of frame annealing or vibratory stress relief.
Have them calculate the springback compensation difference for high strength steel, stainless steel, and aluminum under the same V-die opening, and give corresponding tonnage recommendations. If the answer is only that they can bend everything without specific parameters for material thickness and tensile strength, their experience is limited.
If the shop lacks in-house repair capability, a local supplier's response speed is usually worth the price difference. With a cheap overseas machine, if a hydraulic valve or servo drive fails, waiting for parts can exceed a month. A compromise is to choose an overseas brand but with an authorized local service provider.
Calculate energy consumption, tooling wear, operator efficiency, scrap rate, and expected repair costs over three years. A cheaper machine that only completes 80 percent of the parts per hour compared to an older machine may actually cost more. Require the supplier to provide a cycle time demonstration for typical workpieces.
At a minimum, there should be laser safety protection or light curtains, two-hand operation stations, anti-drop hydraulic locks, and reasonably placed emergency stops. Also confirm that foot switches have anti-accidental covers and that back gauge movement does not create pinch hazards. Safety levels should meet current local standards rather than versions from five years ago.
Bring your three most commonly used sheet materials to the supplier's demonstration area, bend 20 pieces consecutively, and measure the angle deviation of the first, middle, and last pieces. Repeat positioning accuracy should be checked both before and after machine warm-up and with different operators, not just from no-load numbers.
Conclusion
When evaluating an econom press brake supplier, the first thing to watch is whether precision holds up after hundreds of thousands of cycles. A machine that bends accurately on day one but drifts under sustained workload will quietly erode your margins. Ask about frame rigidity, ram guiding systems, and how the supplier tests repeatability over time—not just during a demo. Equally important is build quality you can actually see before signing. A trustworthy partner will encourage you to inspect welds, thickness of side frames, and the quality of hydraulic or electrical components in person. If they hesitate or only offer glossy brochures, that is a red flag. Support is another non-negotiable. Delivery is not the finish line; you need a team that helps with installation, offers operator training, and can ship replacement parts quickly when a job is waiting. The best suppliers treat your first breakdown as their problem too, not just a warranty claim.
Unusual bending jobs often expose the difference between a generic machine and a supplier that listens. Whether you need custom tooling, extended stroke, special back gauge fingers, or offline programming for complex profiles, a reliable partner will adapt the press brake to your parts rather than forcing your parts to fit the machine. Delivery timelines also deserve as much scrutiny as the hardware. A realistic supplier will map out production, testing, and shipping milestones against your own production plan, and they will flag potential delays early instead of overpromising. Finally, look for a proven track record in real workshops, not just trade show displays. Ask for references from shops that run similar material thicknesses and batch sizes. If those operators still praise the machine after three or four years of daily use, you have found more than a vendor—you have a fabrication partner.
Contact Us
Contact Person: James Chen
Email: [email protected]
Tel/WhatsApp: 86 13770803946
Website: https://www.hunsone.com/